Submit Inquiry
27 West Beaver Creek Road Unit #2
Richmond Hill, ON, CANADA L4B 1M8

International:

1-905-886-0335

US & Canada:

1-800-265-5696

7 Best Shot Blasting Equipment for Global Buyers

Choosing the right Shot Blasting Equipment is no longer a simple price comparison. Global buyers must examine cleaning capacity, abrasive recovery, dust control, automation, maintenance access, and energy use. A machine may look powerful on a showroom floor. Its real value appears beside a dusty conveyor, after months of production.

Recent market studies from Grand View Research and MarketsandMarkets indicate steady growth in industrial blasting and surface-treatment equipment. Their findings connect this growth with automotive production, fabricated steel, foundries, shipbuilding, and infrastructure renewal. Demand is increasing for enclosed systems, recyclable abrasives, and more consistent surface profiles. Exact market estimates differ between reports. That difference deserves attention, not dismissal.

As abrasive-blasting specialist Dr. David A. Summers has stated, “Surface preparation is a process, not a single operation.” This principle remains practical. Wheel speed, abrasive size, part geometry, and exposure time must work together. One setting rarely suits every component.

The seven machines reviewed here are not ranked by marketing language alone. They are assessed through working width, throughput, blast-wheel design, media efficiency, operator safety, service support, and documented results. Buyers should also request test samples, noise data, spare-parts lead times, and references from similar factories. Small details matter.

A cheaper machine can become expensive. Fast.

This guide has one limitation: supplier specifications are not always measured under identical conditions. Readers should verify performance independently before purchasing. The best Shot Blasting Equipment is the system that delivers repeatable preparation, controlled operating costs, and reliable results in the buyer’s actual production environment.
7 Best Shot Blasting Equipment for Global Buyers

Shot Blasting Taxonomy: Seven Types, 0.3–2.5 mm Media, 25–500 kg Loads

7 Best Shot Blasting Equipment for Global Buyers

Shot blasting equipment is easier to compare when classified by work handling and load size. Seven common types include pressure-blast cabinets, suction-blast cabinets, tumble-belt machines, rotary-table machines, hanger systems, mesh-belt systems, and roller-conveyor machines. Each design suits a different production rhythm. Cabinets handle smaller batches, often around 25–80 kg. Rotary tables support repeated processing of castings with stable positioning. Hanger systems leave fewer contact marks on complex parts. Tumble-belt machines move many small components together, but fragile edges need careful testing.

Media selection strongly affects the result. Steel shot between 0.3 and 0.6 mm can clean smaller castings and remove light scale. Sizes from 0.8 to 1.5 mm offer stronger impact for general-duty work. Media from 1.8 to 2.5 mm suits heavy castings, thick scale, and aggressive preparation. Larger media can damage thin ribs. That mistake is expensive. Load capacity may range from 25 kg in compact cabinets to 500 kg in heavy conveyor or hanger systems. Actual capacity depends on part shape, not weight alone. A 200 kg load of tangled parts may block circulation. I have seen clean-looking surfaces fail later because hidden pockets received little impact. Trial runs should check coverage, media flow, dust control, and cycle time before purchase. Yet even these checks can miss one issue: operator loading habits often change the final finish.
Wheel-Blast Systems: 50–250 kg/min Throughput for High-Volume Lines

7 Best Shot Blasting Equipment for Global Buyers

Wheel-Blast Systems: 50–250 kg/min Throughput for High-Volume Lines

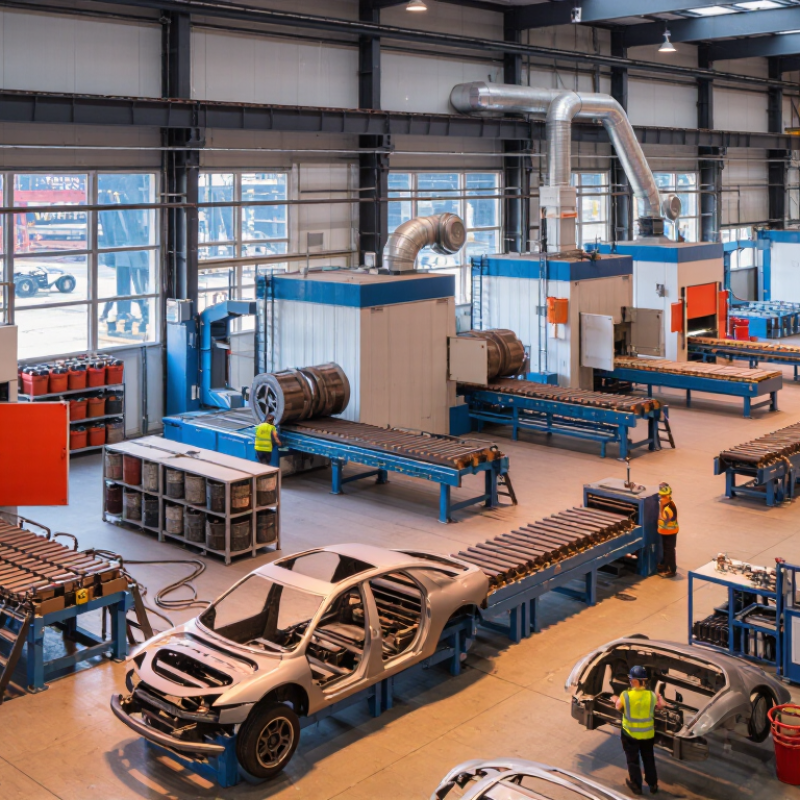
In high-volume metal finishing, wheel-blast systems deserve close attention. Modern machines can process 50–250 kg/min, depending on part geometry, abrasive flow, and surface requirements. That range is substantial. It suits foundries, forging operations, and structural component lines with steady production schedules. A direct conveyor path helps maintain consistent exposure. However, throughput figures should never be judged alone. A dense load of castings may reduce effective cleaning speed.

Experienced buyers inspect the wheel diameter, motor power, chamber layout, and media recovery system. These details affect cleaning uniformity and operating costs. For example, poorly positioned parts can leave shadowed areas inside deep ribs or narrow corners. Automatic tumble or conveyor movement may improve coverage. Strong dust collection is also essential. It protects visibility, equipment, and workplace air quality.

Maintenance planning often decides whether a machine performs reliably after installation. Inspect blast wheels, liners, seals, and elevator belts at scheduled intervals. Keep spare wear parts available near the production area. I have seen lines lose hours because one inexpensive liner was unavailable. That weakness is easy to overlook. Buyers should request verified capacity data using similar parts, media, and loading methods. A system rated at 250 kg/min may perform differently with fragile or irregular components. Careful testing remains wiser than relying on a headline specification.

7 Best Shot Blasting Equipment for Global Buyers

Wheel-blast systems can deliver approximately 50–250 kg/min throughput for high-volume production lines, depending on equipment configuration, part geometry, media flow, and required surface coverage.

The chart shows representative planning capacities for seven common shot blasting equipment configurations. Actual production rates should be verified through part trials and supplier specifications.

Air-Blast Cabinets: 4–8 bar Pressure and 0.5–2.0 m³/min Airflow

Air-Blast Cabinets:
4–8 bar Pressure and 0.5–2.0 m³/min Airflow

Pressure
4–8 bar
Airflow
0.5–2.0 m³/min

Air-blast cabinets are practical for removing rust, scale, paint, and casting residue from smaller parts. A working pressure of 4–8 bar covers many cleaning and surface-preparation tasks. Lower pressure suits delicate surfaces and softer media. Higher pressure helps remove stubborn contamination, but it can increase surface wear. More pressure is not always better.

Airflow matters just as much as pressure. A cabinet using 0.5–2.0 m³/min needs a compressor that can maintain output during continuous blasting. A small compressor may reach 8 bar briefly, then lose pressure under load. That uneven performance creates patchy cleaning and wastes abrasive. Check the nozzle diameter, trigger time, and media type before comparing specifications. The numbers can mislead.

A dependable cabinet should include a pressure regulator, moisture separator, sealed gloves, and effective dust extraction. Moisture in the air line can clog media and leave stains on prepared metal. Visibility also matters. A clear viewing window, internal light, and replaceable protective film make inspection easier. Test a sample part before purchase. I would also question claims based only on maximum pressure, because real workshop performance often depends on airflow stability, nozzle condition, and operator technique. Controls should feel simple, not impressive.

Tumble, Table, and Hanger Machines: 25–500 kg Workpiece Loads

7 Best Shot Blasting Equipment for Global Buyers

Tumble, table, and hanger machines cover different workpiece loads, from 25 to 500 kg. The right choice depends on shape, surface area, batch size, and handling time. Tumble machines suit small, durable castings that can roll together. They often process 25–150 kg per batch. Table machines provide controlled exposure for heavier or fragile parts, commonly around 100–500 kg. Hanger machines keep complex components suspended, reducing shadowed surfaces and contact marks. They are useful for engine housings, frames, and irregular castings.

The 2024 World Foundry Statistics report recorded over 109 million tonnes of global castings in 2023. That volume increases pressure for repeatable cleaning and shorter cycle times. Equipment buyers should check turbine speed, abrasive flow, chamber dimensions, and dust-collection capacity. A machine rated for 500 kg may not handle long parts safely. Geometry matters more than the headline load.

Practical testing is essential. Place a real 25 kg batch inside the chamber, then inspect corners and threaded holes. Do not rely only on catalogue photographs. ISO 8501-1 helps define visual cleanliness grades, but it does not replace process trials. I have seen buyers overestimate tumble capacity and underestimate part damage. That mistake is expensive. Slightly uneven finishes can still appear after correct-looking settings. Record media size, cycle time, and wear after repeated batches.

7 Best Shot Blasting Equipment for Global Buyers - Tumble, Table, and Hanger Machines: 25–500 kg Workpiece Loads
Rank Equipment Type Typical Workpiece Load Recommended Workpiece Profile Typical Chamber or Table Size Blast Wheel Configuration Typical Throughput Common Abrasive Media Indicative Installed Power Best For Main Advantages Key Limitations
1 Batch Rubber-Belt Tumble Blast Machine 25–150 kg per batch Small to medium castings, forgings, fasteners, and heat-treated parts that can tolerate controlled tumbling Approx. 600–1,200 mm belt width; chamber volume commonly 0.15–0.80 m³ 1–2 centrifugal wheels, generally 7.5–22 kW each Approximately 300–1,500 kg/h, depending on part geometry and cleaning standard Steel shot, steel grit, or conditioned mixed media; commonly 0.3–1.2 mm steel abrasive Approximately 20–55 kW, excluding upstream and downstream equipment High-volume cleaning of durable, non-fragile parts Good batch productivity, even exposure, compact layout, and relatively low labor requirement Not suitable for fragile parts, deep cavities, parts that must not contact one another, or easily tangled components
2 Continuous Tumble Belt Shot Blast Machine 50–250 kg per loading cycle or continuous feed Medium-sized castings and forgings with regular production flow and moderate impact resistance Approx. 800–1,500 mm belt width; effective chamber length commonly 1,000–2,500 mm 2–4 centrifugal wheels, typically 11–30 kW each Approximately 800–3,500 kg/h, subject to feed rate and required surface condition Steel shot or steel grit selected according to hardness, profile, and required surface preparation Approximately 45–120 kW, excluding conveyors and dust collection Automated foundry, forging, and general metal-processing lines Supports continuous production, reduces manual handling, and provides high cleaning capacity Requires stable part dimensions and controlled feed; part-to-part contact can cause dents or edge damage
3 Table-Type Shot Blasting Machine 100–500 kg per batch Large, heavy, flat, or delicate components that need separated placement and controlled orientation Rotary table diameter commonly 800–2,500 mm; chamber height often 800–2,000 mm 1–2 centrifugal wheels, commonly 11–30 kW each Approximately 300–2,000 kg/h, depending on loading density and blast coverage Steel shot, steel grit, or a controlled combination for cleaning and surface preparation Approximately 30–90 kW, excluding dust collector and material-handling equipment Large castings, gear housings, welded fabrications, and parts requiring low collision risk Good part visibility, controlled positioning, flexible batch sizes, and reduced part-on-part impact Usually requires manual loading; shadow areas may need repositioning or additional blast passes
4 Single-Hanger Hook Shot Blasting Machine 50–300 kg per hook Medium and large castings, fabricated structures, pipes, and components with lifting points Hook load commonly 50–300 kg; chamber height approximately 1,500–3,500 mm 2–4 centrifugal wheels, typically 11–30 kW each Approximately 250–1,500 kg/h, depending on workpiece shape and blast-cycle time Steel shot for cleaning and peening; steel grit when a more aggressive profile is required Approximately 45–120 kW, excluding lifting and dust-collection systems Parts with complex shapes, cavities, ribs, or surfaces that require individual handling Low part-to-part contact, good access to complex surfaces, and flexible workpiece positioning Lower productivity than continuous systems; loading fixtures and hook balance are important
5 Multi-Hanger Continuous Shot Blasting Machine 150–500 kg per hook or combined batch Medium and large components requiring repeatable, high-volume processing with sequential loading Hook spacing commonly 800–1,500 mm; chamber height approximately 2,000–4,000 mm 4–8 centrifugal wheels, commonly 15–37 kW each Approximately 800–4,000 kg/h, depending on hook spacing, cycle time, and component geometry Steel shot or steel grit matched to the substrate and required surface profile Approximately 100–300 kW, excluding conveyor, lifting, and dust-collection equipment High-volume production of castings, automotive components, and fabricated assemblies Continuous operation, repeatable exposure, reduced handling time, and strong production-line compatibility Higher capital cost and floor-space requirement; workpieces need secure and balanced suspension
6 Rotary Table with Satellite Fixtures 150–500 kg per batch Precision castings, machined parts, and components requiring rotation for improved blast coverage Main table diameter commonly 1,200–2,500 mm; satellite fixtures typically 3–8 positions 2–4 centrifugal wheels, generally 11–30 kW each Approximately 400–2,000 kg/h, depending on fixture density and cycle programming Steel shot, steel grit, or specialized conditioned abrasive for controlled cleaning or peening Approximately 50–140 kW, excluding automation and dust collection Parts needing multiple orientations, consistent coverage, and repeatable process control Improves exposure to recessed areas, limits uncontrolled collision, and supports automated recipes Fixtures require maintenance and part-specific design; setup cost is higher than a basic table machine
7 Hanger-Type Shot Blasting Machine with Rotating Hook 100–500 kg per hook Heavy castings, engine blocks, structural parts, and components with irregular or three-dimensional surfaces Hook load commonly 100–500 kg; chamber height approximately 2,000–4,500 mm 2–6 centrifugal wheels, typically 15–37 kW each Approximately 500–2,500 kg/h, depending on workpiece mass, rotation speed, and blast recipe Steel shot for scale and sand removal; steel grit for heavier surface preparation Approximately 70–180 kW, excluding hoist, conveyor, and dust-collection systems Heavy-duty cleaning where full three-dimensional access and controlled rotation are required Excellent access to multiple surfaces, suitable for heavy loads, and adaptable to mixed component sizes Requires adequate overhead clearance and lifting equipment; cycle times can be longer for dense loads

Note: The figures shown are typical industry ranges for preliminary equipment selection. Actual capacity, power, cycle time, abrasive consumption, and surface results vary with workpiece material, geometry, loading density, abrasive size, required cleanliness, and dust-collection specifications.

Global Buyer Checklist: ISO 8501-1 Sa 2½, CE, and ATEX Compliance

Global buyers should judge shot blasting equipment by verified surface results, not cabinet size alone. Among seven common equipment formats, the right choice depends on part geometry, production volume, and abrasive recovery. ISO 8501-1 Sa 2½ means a very thorough blast-cleaned surface, with only slight staining remaining. Ask suppliers for inspection records, surface photographs, and measured cleanliness results. Visual approval alone can be misleading.

CE compliance requires more than a printed logo. Request the Declaration of Conformity, operating instructions, risk assessment, and safety test records. ATEX compliance needs careful attention when combustible dust or explosive atmospheres may exist. Confirm the intended equipment category, zone classification, dust collector design, grounding, and pressure-relief measures. These details often differ between a workshop and a high-volume production line. A machine may be suitable in one facility but unsuitable in another.

Tips: Check the finished steel under strong, even lighting. Compare it with an agreed Sa 2½ reference image. Measure dust and surface profile before coating. Confirm abrasive containment around doors, seals, and recovery points. Do not accept vague claims such as “fully compliant.” Ask which documents support each claim. I have seen buyers focus on blasting speed and overlook extraction capacity. That mistake can increase maintenance, downtime, and safety concerns. Also review local installation requirements, because imported documentation may not explain every site condition.

123